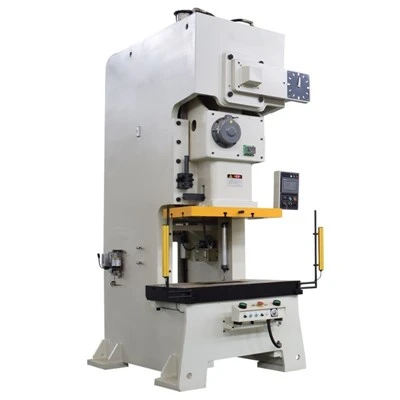
Core Selling Points
■ Uniform knurl pattern with consistent depth around cap circumference
■ Multiple knurl patterns: straight, diagonal, diamond, custom
■ Adjustable knurl depth from 0.1 to 0.5mm
■ High speed processing up to 350 pieces per minute
■ Cold forming process with no material removal
■ Hardened knurl rollers for long service life
■ Automatic cap feeding and orientation
■ Standalone or inline installation capability
Technical Specifications
|
Parameter |
Specification |
|
Model No. |
KP-KN-350 |
|
Production Speed |
150–350 pieces/min |
|
Cap Diameter Range |
Ø20 – 80 mm |
|
Knurl Depth |
0.1 – 0.5 mm (adjustable) |
|
Knurl Pattern |
Straight / Diamond / Custom |
|
Knurl Pitch |
0.5 – 2.0 mm |
|
Power Rating |
3 kW |
|
Overall Dimension |
1000 × 800 × 1500 mm |
|
Total Weight |
Approx. 950 kg |
|
Roller Material |
Alloy tool steel |
|
Control System |
PLC Control |
|
Certification |
CE |
|
Warranty |
2 Years |
Production / Working Process
Step 1: Cap Loading – Caps automatically fed and oriented
Step 2: Cap Centering – Cap positioned between knurling rollers
Step 3: Roller Engagement – Knurling rollers press against cap side
Step 4: Knurl Forming – Rollers rotate and imprint knurl pattern
Step 5: Depth Control – Precision stop at predetermined depth
Step 6: Roller Retraction – Knurling rollers withdraw
Step 7: Cap Transfer – Knurled cap moves to discharge
Step 8: Visual Inspection – Optional pattern verification
Step 9: Next Cycle – Continuous automatic production

Application Scenarios
• ROPP cap side wall knurling
• Screw cap grip texture creation
• Tamper-evident cap anti-slip patterns
• Metal jar lid knurling operations
• Specialty cap decorative texturing
Case Study
■ Customer Background
A spirits bottle manufacturer upgrading their premium wine cap line. They needed diamond knurling on ROPP caps to improve grip and enhance premium appearance for their luxury product range.
■ Project Challenge
• Required sharp diamond knurl pattern on 31.5×18mm ROPP caps
• Knurl depth must be uniform 0.25mm around circumference
• No sharp edges or burrs allowed on finished caps
• Must integrate with existing ROPP production line
■ Our Solution
• Installed KP-KN-350 knurling machine with diamond pattern rollers
• Configured precision depth control with servo adjustment
• Designed integration interface for existing production line
• Specified polished roller teeth for burr-free knurling
■ Result & Benefits
• Diamond knurl pattern sharp and uniform around full circumference
• Knurl depth consistently maintained at 0.24–0.26mm
• Zero burrs detected in quality inspection
• Seamlessly integrated running at 220 caps/min line speed
Frequently Asked Questions (FAQ)
Q: What is the purpose of cap knurling?
A: Knurling creates textured surface on cap side wall to improve grip and increase friction, making caps easier to twist open by hand.
Q: What knurl patterns are available?
A: Common patterns include straight knurl, diagonal knurl, diamond knurl and custom decorative patterns.
Q: Does knurling affect cap wall thickness?
A: Knurling displaces material rather than removing it, so wall thickness remains essentially unchanged.
Q: How deep should knurling be for good grip?
A: Typical knurl depth ranges from 0.15mm to 0.35mm for most beverage caps. Deeper knurls provide better grip.
Q: Can knurling be done on tapered cap sides?
A: Yes, with specially profiled knurling rollers matched to cap taper angle.
Q: How long do knurling rollers last?
A: Hardened steel knurling rollers typically last 8–15 million pieces under normal operating conditions.
Hot Tags: cap knurling machine, China cap knurling machine manufacturers, factory